Wrap-around and front-and-back labelling are two configurations of automatic self-adhesive labelling machines. Both apply pressure-sensitive labels supplied on a release liner: the label applicator draws the liner around a peel plate, the label separates, and the machine transfers it to the passing container. The difference lies in how the machine handles the container and where the labels end up.
A wrap-around machine rotates the container so that one label follows its circumference. A front-and-back machine keeps the container stable while two applicators place separate labels on opposite faces. The choice depends mainly on container geometry, the required label layout, production output, and the number and frequency of format changes. This article compares them on those terms, for self-adhesive labelling only.
How Wrap-Around Labelling Machines Work
Containers travel upright on a conveyor and pass through a spacing device, such as a spacing wheel or feed screw. A sensor detects each container and triggers the label applicator, which dispenses the label so that its leading edge meets the container as it enters the wrapping station.
In the most common arrangement, the wrapping station has a driven wrap-around belt on one side of the conveyor and a fixed counterpressure plate on the other. The belt pushes the container along the plate, so it rolls as it travels forward. The label follows the rotating surface, and the belt and plate press it on. An alternative is a roller system, which holds the container between rollers and rotates it in a defined position. Because rollers stabilise the container in one place, this arrangement gives more direct control over rotation, which can help with containers that are not true cylinders.
These machines handle full-wrap and partial-wrap labels on cylindrical bottles, jars, cans and other round containers. A full-wrap label covers the entire circumference, usually with a short overlap. A partial-wrap label covers only part of it, for example a front panel extending around the sides.
Controlled rotation is the core requirement. The surface speed of the container must match the dispensing speed of the label. If the container slips against the belt or wobbles on the conveyor, the label can skew, wrinkle or trap air. Container stability therefore matters as much as applicator precision.
Label alignment also depends on the labelling area. The label must sit on a section that is cylindrical over the full label height. On a tapered section, the circumference differs between the top and bottom of the label, so a rectangular label runs off-line as it wraps. The height of the straight panel limits label height, and the circumference limits label length. Diameter variation changes a full-wrap overlap directly: each millimetre of diameter changes the circumference by roughly 3.1 mm. The label design therefore needs an overlap that works across the container’s production tolerance.
Some applications require the label to sit relative to a container feature, such as a handle, mould seam or embossing. A standard wrap-belt machine does not locate the container angularly, so the label starts at an arbitrary point on the circumference. Orientation needs additional equipment: typically a sensor that detects the feature or a reference mark, and a controlled rotation station that turns each container to a defined angle before application. This adds complexity, so specify it only where the packaging design needs it.
How Front-and-Back Labelling Machines Work
A front-and-back labelling machine uses two label applicators on opposite sides of the conveyor. The container receives a front label and a back label in one pass. The labels usually come from separate reels, which allows different sizes, materials or artwork on each side.
Container handling determines placement quality. A spacing device sets a consistent pitch, so each applicator can dispense a complete label before the next container arrives. An alignment system, such as side belts or chains, squares flat and oval containers to the direction of travel, so each face runs parallel to its applicator. Side guides keep containers centred between the applicators. Where fitted, a top hold-down belt runs in synchronisation with the conveyor and bears on the container from above, stopping tall, light or unstable containers from tipping or twisting. Pressing devices such as brushes, rollers or foam-faced belts then wipe the labels down.
This configuration suits flat-sided, oval, square and rectangular containers, because each face offers a defined surface and the container does not need to rotate. An oval face curves in one direction only, and a label can follow it if the label material is conformable enough for the radius. Faces curved in two directions, or with recesses, are more demanding.
Round containers can turn on the conveyor, so nothing fixes where the two labels land relative to each other or to container features. Round formats therefore need handling that prevents rotation, such as side belts that grip the container, or a wrap-around module that applies the labels during controlled rotation. Alignment with a handle or seam also requires orientation equipment.
The height and angle of each applicator set the vertical position of its label. The dispensing delay after the container sensor sets each label’s position along the container. On flat containers, the two labels can therefore sit symmetrically or offset from each other.
Scope of supply varies. Alignment belts, a top hold-down belt, orientation, a wrap-around module, coding units and vision inspection may be standard on one machine and optional on another, so buyers should confirm the exact scope.
Wrap-Around vs Front-and-Back Labelling: Key Differences
The table compares both configurations.
COMPARISON OF LABEL TYPES
| CRITERION | WRAP-AROUND | FRONT-AND-BACK |
| Container geometry | Cylindrical, with a straight labelling panel | Flat-sided, oval, square, rectangular; round formats need extra handling |
| Label coverage and placement | One label, full wrap or partial wrap | Two separate labels on opposite faces, set independently |
| Rotation or stabilisation | Controlled rotation by belt and counterpressure plate, or rollers | No rotation; alignment, side guides, top hold-down belt where fitted |
| Applicator arrangement | Usually one applicator | Two applicators on opposite sides |
| Format changeover | Applicator, wrapping station gap, spacing device, guides | Both applicators, alignment, guides, top belt, pressing devices |
| Production output | Depends on diameter, label length, rotation, spacing | Depends on pitch, label length, stability, handling |
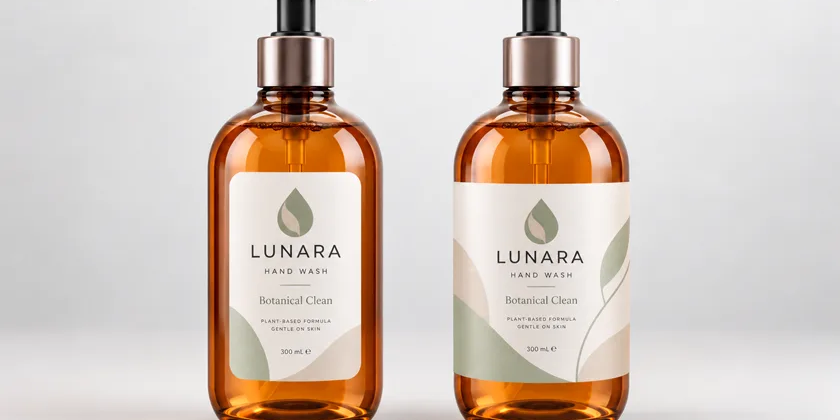
Label count alone does not determine the appropriate machine. A wrap-around machine can apply front and back labels to a round container, supplied on one liner and placed during a single rotation. A front-and-back machine can run with one applicator to label a single face. What decides is how the container behaves in handling and where the labels must sit.
Changeover effort tends to follow the number of adjustment points. A front-and-back machine has two applicators and more handling elements to reset, so a format change involves more settings. Position indicators and stored recipes reduce, but do not remove, this effort. Where formats require change parts, such as a feed screw for each container, the parts inventory grows with the range.
Some front-and-back machines can incorporate an optional wrap-around module for round containers. This broadens the container range, but buyers should check the module’s diameter range, maximum label length and orientation capability against the actual formats.
Neither configuration is universally faster, more accurate, more compact or cheaper. Output depends on container size and stability, label length, spacing and the rest of the line. Placement accuracy depends on container tolerances and label material as much as on the applicator. A comparison is meaningful only for specific equipment running specific containers and labels.
Which Configuration Is Right for Your Production?
A sound selection starts with the physical inputs, not with the machine type. Container samples should come from normal production, because tolerances in diameter, ovality and wall straightness affect wrapping and alignment. Drawings should show the labelling area, including the straight panel height and any taper, shoulder or feature that affects placement. The label specification should define size, material, liner, reel dimensions, winding direction and position on the container, and state whether labels must align with a feature or with each other.
Required output should be the sustained figure the line needs, in containers per minute. Nominal machine speed is not the same as achievable output, which also depends on container size, label length and upstream supply. The number of formats and changeover frequency determine how much adjustment time production can accept, while available line space and transfer arrangements determine what fits.
A dedicated wrap-around labelling machine may suit a range of cylindrical containers that need full-wrap or partial-wrap labels. Each changeover involves one applicator and one wrapping station. If some formats need placement relative to a handle or seam, orientation should be in the specification from the start.
A front-and-back machine may suit containers with flat or oval faces that carry separate labels on opposing sides, such as a branded front label and a back label with product information. Container stability and alignment then become the key handling requirements.
A combined configuration, usually a front-and-back machine with a wrap-around module, may suit a mixed range of flat, oval and round containers. It can avoid a second machine and its line space, at the cost of more operating modes and changeover settings. It is most practical when the production schedule allows switches between container types without unacceptable downtime.
Whatever the configuration, trials should confirm the choice. Running the intended containers and labels on the proposed machine, or an equivalent, shows whether labels sit without skew, wrinkles, air bubbles or flagging. It also shows whether placement meets the specified tolerance and what output the machine achieves under realistic conditions. Including containers from both ends of the tolerance range gives a firmer basis for the decision than any general comparison.